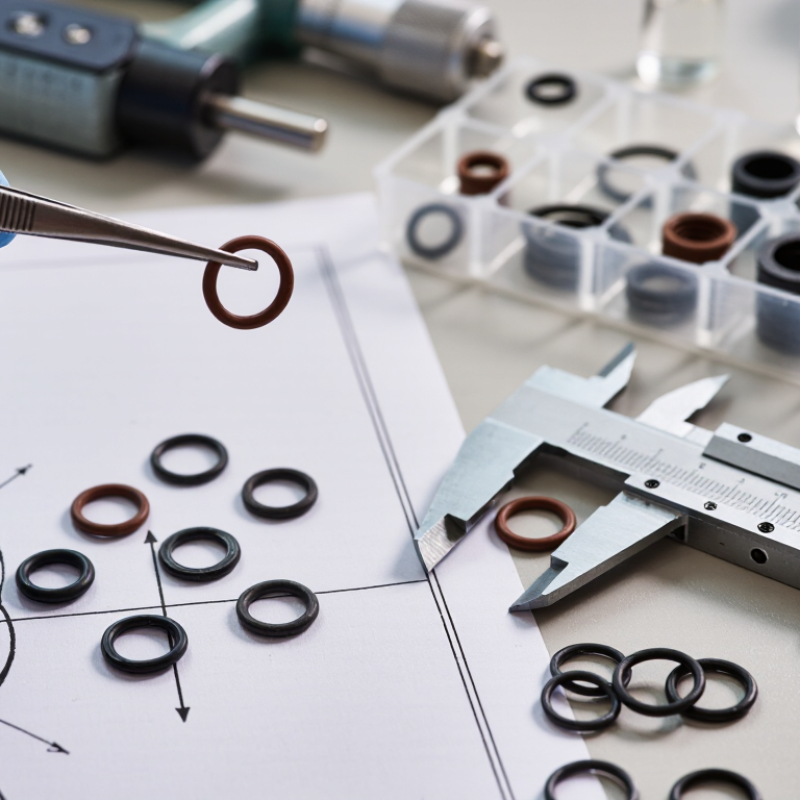
Choosing Tiny O Rings for global sourcing requires more than comparing prices on a spreadsheet. These small components can control pressure, prevent leakage, and protect sensitive assemblies. A ring measuring only a few millimeters may face heat, vibration, chemicals, compression, and repeated movement.
Dr. Robert Flitney, a recognized sealing specialist and author of The Sealing Handbook, states, “A seal must be selected for the application, not merely for the groove.” This principle remains practical for international procurement. Buyers should confirm the required inside diameter, cross-section, hardness, material, tolerance, and operating temperature. They should also review chemical compatibility and compression-set performance. A low-cost NBR option may suit clean air, but it may fail quickly beside aggressive oils or high heat.
Small details matter.
Global sourcing adds another layer of risk. Suppliers may use different material codes, inspection methods, or packaging practices. Requesting technical data sheets, batch records, dimensional reports, and sample approvals can expose these differences early. Independent testing may be worthwhile for safety-critical assemblies. However, laboratory results alone cannot replace production experience. A sample can perform well while a large batch reveals inconsistent curing or poor surface finish.
That assumption can fail.
A reliable sourcing process therefore combines engineering judgment, supplier audits, traceability, and realistic testing. It should also leave room for doubt. Tiny O Rings are simple in appearance, yet their reliability depends on the entire sealing system. This guide examines how to compare suppliers, validate specifications, and make a more defensible global purchasing decision.
Tiny O-rings need a precise specification before suppliers can quote consistently. Define the cross-section first, usually between 0.5 and 1.0 mm. Then record the inside diameter, material, hardness, and operating temperature. Small errors matter. A 0.05 mm variation can affect compression, installation, and sealing performance.
Use ISO 3601 as a reference for dimensions, tolerances, and quality expectations. However, do not assume every miniature size fits a standard series. Check the exact size designation and confirm whether the requested 0.5–1.0 mm section is covered. Ask for inspection records, dimensional sampling methods, and material certificates. For critical applications, specify surface defects, flash limits, and acceptable deformation.
Sourcing decisions should also reflect the real environment. Identify contact fluids, pressure, motion, assembly tools, and storage conditions. A soft compound may seal easily but fail under pressure. A harder compound may resist extrusion but require more assembly force.
Prototype testing is essential. Yet a checklist can still miss an installation issue. Measure twice. Review the groove design with the supplier, especially when tools, cavities, and inspection equipment differ across countries. Clear drawings and controlled tolerances reduce misunderstandings, but they cannot replace physical validation.
Selecting tiny O rings for global sourcing starts with the seal geometry, not the supplier catalog. Measure the groove and mating shaft with calibrated tools, then match the ring’s inside diameter and cross-section. A ring that is only 0.2 mm too large may roll during assembly. One that is too small can stretch excessively and lose contact.
70 Shore A hardness often suits compact static seals because it balances flexibility and resistance to extrusion. However, hardness alone does not confirm performance.
Check the groove depth, squeeze percentage, pressure, temperature, and fluid exposure. For example, a narrow groove may need a softer ring, while higher pressure may require stronger support.
Ask for dimensional tolerances, material data, batch traceability, and inspection records. Request samples from more than one production batch when consistency matters.
Test the actual seal design.
I have seen drawings look correct while the assembled ring pinched at one corner. That mistake was not caused by hardness alone; the groove edge was too sharp.
Rounded edges, clean surfaces, and controlled lubrication can matter just as much. During global sourcing, confirm measurement standards and tolerance units clearly.
Metric and imperial sizes can appear nearly identical, but they may not seal reliably. A useful design review should challenge the first size choice rather than simply approve it.
Choosing tiny O-rings for global sourcing starts with the media and temperature profile. NBR suits mineral oils, fuels, and pneumatic systems. Its typical working range is –30°C to 100°C. FKM handles many aggressive oils, fuels, and high-temperature fluids. Its usual range is –20°C to 200°C.
These limits are practical guides, not guarantees. A 2024 rubber industry report from the International Rubber Study Group places global synthetic rubber production above 15 million metric tonnes annually. That scale supports broad material availability, but compound quality still varies between suppliers. ASTM D2000 classifications help compare elastomer performance, while ISO 3601 defines important O-ring dimensional and acceptance requirements. Ask for batch certificates, hardness data, and compression-set results.
Media compatibility deserves closer attention. Water, steam, solvents, vacuum, and bio-based oils can change the selection quickly. For example, NBR may swell in certain fuels, while FKM can lose flexibility in cold conditions. Actual pressure, cycling, surface finish, and squeeze also matter. A neat temperature chart can mislead. Test samples at the real temperature, pressure, and fluid exposure. Small rings need careful inspection; one tiny surface cut can create a large leak. I would also question suppliers offering “universal” compounds. That claim sounds convenient, but it often hides compromises.
Select the elastomer according to the working media and temperature range. The chart shows typical continuous service-temperature ranges for NBR and FKM compounds.
NBR is commonly selected for mineral oils, fuels, and general-purpose sealing from approximately −30°C to 100°C. FKM generally provides a wider high-temperature range, approximately −20°C to 200°C, and stronger resistance to many fuels and chemicals. Actual limits depend on compound formulation, pressure, media, and exposure time.
Tiny O rings require more than a quick diameter check. Before ordering, confirm the inside diameter, cross-section, and dimensional tolerance. A difference of a few hundredths of a millimeter can change sealing pressure. Ask the supplier which measurement tools and inspection standards they use. Digital calipers may be unsuitable for very small sections. Optical measurement is often more reliable.
Compression needs equal attention. Calculate the squeeze against the actual groove, not a simplified drawing. Check gland depth, stretch, clearance, and extrusion risk at operating pressure. Material hardness also affects assembly force and recovery. Test samples across the expected temperature range. A seal that works at room temperature may leak after heating, cooling, or repeated movement. Real conditions matter.
Leakage testing should match the application. Use the intended fluid, pressure, temperature, and hold time whenever possible. Inspect multiple samples, including parts from different production batches. I have found that a perfect first sample can create false confidence. It is only one data point. Request test records, material certificates, and traceable batch information before approving volume production. Packaging deserves attention too; tiny rings can deform, dry out, or become mixed during international shipping. A clear acceptance plan reduces misunderstandings between engineering, purchasing, and the supplier. Still, no checklist replaces physical verification. Recheck the design when field results disagree with laboratory data.
Choosing tiny O rings for global sourcing requires more than checking dimensions and price. A practical audit should connect each shipment to a production lot, compound batch, cure date, inspection record, and approved drawing. Ask suppliers to show how one carton can be traced backward within minutes. Missing links are warning signs.
The 2023 MHI Annual Industry Report surveyed more than 1,300 supply-chain professionals. It reported that 55% planned to adopt artificial intelligence within five years. That trend makes digital traceability valuable, but software cannot repair weak records. Request controlled electronic logs, revision histories, retained samples, and corrective-action evidence. PPAP documentation should cover dimensional results, material certification, process flow, control plans, and capability studies where required. Do not accept a polished packet with unexplained gaps.
ASTM D2000 compliance needs careful reading. The supplier should identify the exact material designation, hardness range, temperature limits, fluid resistance, and test methods used. Compare the certificate with independent test results from the same lot. Also verify sampling rules and laboratory calibration. One overlooked detail matters: an O ring can meet size requirements yet fail after heat, compression, or chemical exposure. I would also audit subcontractors, packaging labels, and change-notification procedures. Global sourcing is rarely perfect. That is precisely why every assumption should be recorded and challenged.
| Audit Dimension | What to Verify for Tiny O-Rings | Objective Evidence to Request | Practical Acceptance Criteria | Priority |
|---|---|---|---|---|
| Material identification | Confirm the elastomer family, compound designation, cure system, hardness target, color, and applicable temperature or fluid requirements. | Approved material specification, compound identification record, certificate of analysis, and retained compound sample. | The material description must be consistent across the purchase order, drawing, inspection report, and certificate. | Required |
| ASTM D2000 applicability | Check that the selected rubber specification is written as an ASTM D2000 callout when automotive-style classification is required. | Complete ASTM D2000 line callout, including polymer type, grade, hardness, tensile or elongation requirements, and applicable suffix requirements. | Do not accept the phrase “ASTM D2000 compliant” without a defined callout and corresponding test results. ASTM D2000 does not define one universal compound for every O-ring application. | Required |
| Hardness control | Verify nominal elastomer hardness and the test method used. Small cross-sections can make hardness testing more sensitive to specimen geometry. | Hardness report using an applicable durometer method, test temperature, specimen details, and lot number. | Measured hardness falls within the drawing or material specification tolerance; the test method is consistent between supplier and buyer. | Required |
| Dimensional capability | Measure inside diameter, cross-section, flash, parting-line mismatch, surface defects, and deformation after molding. | First-article inspection report, calibrated optical measurement records, capability study, and representative sample parts. | All critical dimensions meet the approved drawing. The measurement system must resolve the specified tolerance and be suitable for miniature geometry. | Required |
| Measurement system analysis | Assess whether gauges, optical systems, fixtures, and operators can produce repeatable and reproducible measurements. | Gauge calibration certificates, repeatability and reproducibility study, resolution statement, and fixture validation. | Gauge resolution should be appropriate to the tolerance; measurement uncertainty must not obscure conformity decisions. | Recommended |
| Lot definition | Determine how the supplier defines one production lot, including compound batch, mold, cavity, cure batch, and production date. | Written lot-definition procedure, batch traveler, molding record, and packaging label format. | Every shipped quantity can be linked to a clearly defined production lot without relying only on shipment date. | Required |
| Lot traceability | Trace finished parts backward to raw material, compound batch, mold or cavity, process conditions, inspection results, and operators or equipment where applicable. | Traceability matrix, electronic or controlled paper records, batch labels, inspection logs, and nonconformance history. | The supplier can retrieve all relevant records for a selected lot within an agreed response period, such as one business day. | Required |
| Traceability retention | Confirm how long production, inspection, material, and shipment records are retained. | Document-control procedure and retention schedule covering certificates, process records, test data, and complaints. | Retention period meets the buyer’s contract, regulatory, and product-life requirements; records remain legible and protected from unauthorized changes. | Recommended |
| PPAP readiness | Evaluate the supplier’s ability to prepare production-part approval documentation before mass production or design changes. | Design records, engineering change records, process flow, process FMEA, control plan, dimensional results, material results, capability data, and sample parts. | Required PPAP elements are complete, internally approved, and consistent with the latest drawing revision and process flow. | Required |
| PPAP submission level | Agree on the required submission level before tooling release or production approval. | Signed customer-specific PPAP requirement, submission checklist, and approval status. | The supplier follows the buyer’s specified level. PPAP levels are customer-defined submission packages, not automatic evidence of product performance by themselves. | Required |
| Process control | Review control of molding temperature, pressure, cure time, deflashing, cleaning, sorting, and packaging. | Process flow chart, control plan, machine parameter records, reaction plan, and production check sheets. | Critical process parameters have defined limits, inspection frequency, responsible personnel, and documented escalation actions. | Required |
| Cure verification | Confirm that cure state is controlled and that under-cure, over-cure, or inconsistent post-curing cannot pass unnoticed. | Rheometer or cure-curve records, oven records when post-cure is used, and periodic physical-property results. | Cure settings and acceptance limits are documented and linked to the compound batch and production lot. | Recommended |
| Tensile and elongation | Verify that tensile strength and elongation requirements are tested using the method specified by the material standard or customer specification. | Laboratory report referencing the applicable ASTM D2000 requirement and the test method used, commonly ASTM D412 where specified. | Results meet the defined material grade and suffix requirements; test specimens and conditioning are documented. | Required |
| Compression set | Assess resistance to permanent deformation under the specified temperature, time, and compression conditions. | Compression-set report referencing the applicable specification and test method, commonly ASTM D395 where specified. | Results meet the customer’s defined limit at the required temperature and duration; conditions are not reported as a single unexplained percentage. | Required |
| Fluid and environmental resistance | Match the compound to the actual media, temperature, pressure, exposure time, and sealing duty cycle. | Fluid-immersion data, volume or mass-change results, hardness change, tensile retention, and application-specific validation samples. | Acceptance limits are defined for the actual service fluid. Generic “oil resistant” or “chemical resistant” claims are not sufficient. | Required |
| Surface and cleanliness inspection | Check flash, nicks, cuts, blisters, inclusions, mold deposits, lubricant residue, and particles that could affect sealing. | Visual inspection standard, defect limit samples, inspection lighting requirements, sorting records, and cleanliness results when required. | No defect exceeds the approved visual standard or drawing requirement. Critical sealing surfaces receive defined inspection coverage. | Required |
| Sampling plan | Define sample size, inspection frequency, acceptance number, and treatment of destructive tests. | Approved sampling plan based on lot size, risk, criticality, and applicable statistical rules. | Critical dimensions and defects have stricter controls than routine characteristics; sampling rules are documented before production. | Recommended |
| Packaging and shelf life | Protect miniature O-rings from ozone, ultraviolet exposure, heat, contamination, compression, and uncontrolled aging during international shipment. | Packaging specification, manufacturing date or lot date, storage conditions, shelf-life statement, and shipping validation where needed. | Parts are packaged to prevent deformation and contamination; storage conditions and shelf-life limits are clearly identified. | Required |
| Change control | Control changes to compound, raw-material source, mold, cavity, tooling, process parameters, inspection method, and manufacturing location. | Engineering-change procedure, customer-notification workflow, change history, and requalification records. | No material, tooling, process, or site change is implemented without documented risk review and the required customer approval. | Required |
| Nonconformance and corrective action | Review how the supplier contains defective lots, identifies affected shipments, determines root cause, and verifies corrective action. | Nonconformance reports, containment records, root-cause analysis, corrective-action evidence, and effectiveness checks. | Defective material can be quarantined by lot, customer notification is time-bound, and corrective actions are verified with objective evidence. | Required |
| Supplier audit decision | Classify the supplier based on evidence quality, process capability, traceability, and open risks. | Completed audit checklist, risk register, corrective-action plan, and approval decision. | Approve only when critical gaps are closed or formally risk-accepted with a due date, owner, containment plan, and verification method. | Required |